
Modern production and handling facilities need conveyor systems that can adapt to changing workloads, product types, and operating conditions. A modular belt conveyor offers this flexibility through a belt constructed from interconnected plastic modules. Its practical design makes it suitable for industries that require dependable product movement, easy maintenance, and customized conveyor layouts.
What Is a Modular Belt Conveyor?
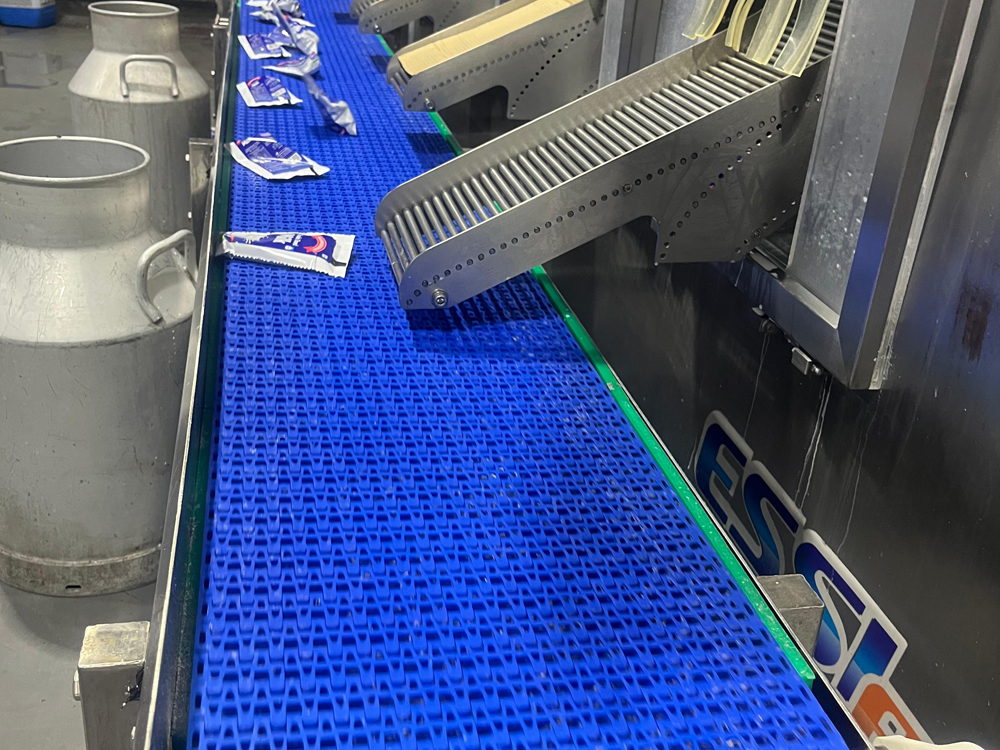
A modular belt conveyor uses a belt made from individual interlocking sections rather than one continuous piece of flexible material. These modules are connected with rods, allowing the belt to form a continuous conveying surface while remaining relatively easy to repair or replace.
The conveyor normally consists of a modular belt, drive sprockets, return components, support frame, motor, and control system. Depending on the application, it can be configured as a straight, inclined, curved, or specialized conveying system.
Different module designs can provide smooth, textured, perforated, or high-grip surfaces according to the requirements of the products being transported.
How Does It Operate?
The motor turns the drive sprockets, which engage with the modular belt and move it along the conveyor frame. Products are placed on the belt at the loading point and carried toward the required destination.
Because the belt is positively driven by sprockets, it can provide controlled movement when properly designed and maintained. Belt width, conveyor speed, support arrangement, and module style can be selected according to product characteristics and operating conditions.
For inclined applications, cleated modules or suitable surface designs can help keep products positioned during movement.
Where Are Modular Belt Conveyors Used?
A modular belt conveyor is commonly used in manufacturing, packaging, food processing, beverage production, logistics, and general material handling. In packaging facilities, it can transfer cartons, containers, and packaged products between different processing stages.
Food and beverage operations may use suitable food-grade modular belt materials for applications involving regular cleaning requirements. Manufacturing plants can use these conveyors to move components and finished products through assembly and inspection areas.
They can also be integrated with equipment such as filling machines, labeling units, packaging machines, inspection systems, and sorting equipment.
Key Benefits of Modular Construction
One of the major advantages of a modular belt conveyor is its repair-friendly construction. If a section of the belt becomes damaged, individual modules or selected sections can often be replaced instead of replacing the complete belt. This can simplify maintenance and reduce unnecessary downtime when the system is properly designed.
The belt design also provides flexibility for different conveyor layouts. Curved configurations can help products change direction without requiring multiple separate conveyor sections.
Modular belts can be selected with different surfaces and opening patterns. This allows businesses to match the conveyor to specific product handling, drainage, cleaning, or grip requirements.
Factors to Consider Before Installation
Choosing the right modular conveyor requires careful evaluation of the application. Consider the dimensions, weight, shape, and surface of the products being transported. Operating temperature, moisture, cleaning chemicals, and hygiene requirements should also influence the choice of belt material.
Other factors include conveyor length, width, speed, incline angle, load capacity, available floor space, and expected operating hours. If the conveyor will connect with automated machinery, its speed and controls should be compatible with the surrounding equipment.
Maintenance and Safe Operation
Regular maintenance helps extend conveyor life and maintain consistent performance. Operators should inspect modules, connecting rods, sprockets, bearings, and support components for signs of wear or damage.
The belt should be kept clean and correctly aligned, while excessive product buildup should be avoided. Following the manufacturer’s recommendations for tension, cleaning, lubrication, and component replacement can help prevent avoidable problems.
Workers should also remain clear of moving parts and use approved isolation procedures before maintenance or cleaning work.
Conclusion
A modular belt conveyor combines adaptable design with practical maintenance advantages, making it suitable for a wide range of industrial applications. Its replaceable belt modules, customizable surfaces, and flexible configurations allow businesses to create conveying systems suited to different products and environments. With proper selection, installation, and maintenance, modular conveyors can support reliable material movement and efficient production workflows.
About The Author